


Blog 
China Top 10 Flue Gas Desulfurization Equipment Suppliers?
China’s Top 10 Flue Gas Desulfurization Equipment Suppliers deserve careful attention as industries reduce sulfur dioxide emissions. Power plants, cement factories, steel mills, and chemical facilities increasingly require dependable pollution-control systems. However, supplier rankings should not rely on production volume alone.
Performance depends on limestone quality, gas temperature, chloride concentration, moisture control, and maintenance support. A polished showroom cannot replace stable operation beside a real absorber tower. John S. Srivastava, an environmental engineer associated with U.S. EPA technical guidance, wrote, “The most common type of FGD system is the wet scrubber.” His observation remains relevant because wet systems still offer strong removal efficiency for large combustion units.
Yet, the “best” supplier is rarely universal. One factory may need a wet limestone scrubber, while another may benefit from a semi-dry or dry system. Energy use matters. So do corrosion-resistant materials, spray-nozzle design, slurry circulation, and gypsum handling. A cheaper quotation may create higher costs later through scaling, leaks, or difficult spare-part sourcing.
This guide examines ten Chinese suppliers through practical criteria. These include engineering experience, reference projects, testing capability, customization, after-sales service, and documented emission performance. Some companies may appear impressive but provide limited public operating data. That is a weakness worth acknowledging.
Buyers should request site references, process guarantees, maintenance records, and clear warranty terms. They should also verify compliance with local environmental requirements before signing contracts. Reliable Flue Gas Desulfurization Equipment is not merely a catalog product. It is a long-term operating system, shaped by engineering decisions, plant conditions, and disciplined service.
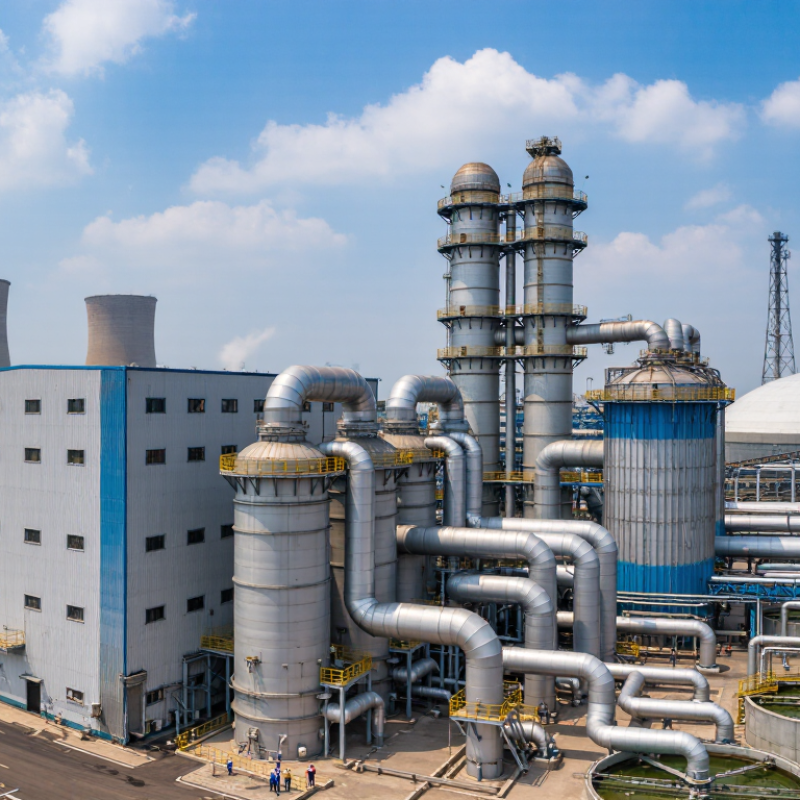
China’s Top 10 Flue Gas Desulfurization Equipment Suppliers
China’s Top 10 Flue Gas Desulfurization Equipment Suppliers
China remains a major market for flue gas desulfurization equipment. The IEA’s Coal 2023 report identifies China as the world’s largest coal-power market. China Electricity Council data also shows continued investment in cleaner thermal generation. These conditions support strong demand for limestone-gypsum, seawater, and dry-sorbent systems.
A practical top-ten assessment should examine installed capacity, sulfur dioxide removal efficiency, project references, spare-part support, and commissioning records. Many Chinese suppliers serve large utility plants, steel mills, cement factories, and industrial boilers. Mature systems can achieve over 95% sulfur dioxide removal when designed and operated correctly. Actual performance depends on coal chemistry, absorbent quality, gas volume, and maintenance. A perfect ranking is impossible. Some performance data remain private.
Tips: Request verified operating data from comparable plants. Check absorber corrosion protection, pump redundancy, mist eliminator design, and wastewater handling. Ask for measured outlet emissions, not only laboratory claims. The U.S. EPA’s Air Pollution Control Cost Manual notes that operating costs can strongly affect lifetime value. Therefore, buyers should compare energy use, limestone consumption, water demand, and replacement intervals. A lower purchase price may become expensive after several years.
China Top 10 Flue Gas Desulfurization Equipment Suppliers? - China’s Top 10 Flue Gas Desulfurization Equipment Suppliers
| Rank | Anonymous Supplier Profile | Primary FGD Technology | Typical Industrial Application | Typical SO2 Removal Efficiency | Indicative Gas-Flow Range | Main By-Product | Common Compliance Reference |
|---|---|---|---|---|---|---|---|
| 1 | Supplier Profile A | Wet limestone–gypsum scrubber | Large coal-fired power stations and industrial boilers | 95–99% | 100,000–3,000,000 Nm³/h | Gypsum | China GB 13223; EU Industrial Emissions Directive |
| 2 | Supplier Profile B | Wet limestone–gypsum absorber with spray towers | Ultra-low-emission power and cogeneration plants | 96–99.5% | 200,000–2,500,000 Nm³/h | Saleable gypsum | China GB 13223; ISO 9001 quality systems |
| 3 | Supplier Profile C | Semi-dry circulating fluidized-bed scrubber | Waste-to-energy plants and medium-sized boilers | 90–98% | 30,000–800,000 Nm³/h | Dry calcium sulfite/sulfate residue | China GB 18485; EU Waste Incineration requirements |
| 4 | Supplier Profile D | Dry sorbent injection | Small boilers, process heaters, and retrofit projects | 50–90% | 10,000–500,000 Nm³/h | Spent lime or sodium-based sorbent | China GB 13271; site-specific permit limits |
| 5 | Supplier Profile E | Spray dry absorber | Industrial boilers and plants requiring moderate water use | 85–95% | 20,000–600,000 Nm³/h | Dry calcium-based residue | China GB 13271; EN 14791 measurement methods |
| 6 | Supplier Profile F | Seawater flue gas desulfurization | Coastal power and industrial facilities | 90–98% | 100,000–2,000,000 Nm³/h | Treated sulfate-rich seawater | Marine discharge permit; China GB 13223 |
| 7 | Supplier Profile G | Dual-alkali wet scrubber | High-sulfur fuels and non-ferrous metallurgy | 95–99% | 50,000–1,000,000 Nm³/h | Sodium/calcium sulfite and sulfate liquor | China GB 31573; local emission permits |
| 8 | Supplier Profile H | Ammonia-based wet scrubbing | Facilities seeking ammonium sulfate recovery | 95–99% | 30,000–700,000 Nm³/h | Ammonium sulfate | China GB 13223; ammonia-safety regulations |
| 9 | Supplier Profile I | Compact wet scrubber package | Cement, glass, chemical, and marine exhaust systems | 90–98% | 5,000–250,000 Nm³/h | Sulfur-bearing wastewater or sludge | China GB 4915; IMO MARPOL Annex VI where applicable |
| 10 | Supplier Profile J | Integrated FGD and dust-control system | Industrial furnaces, sintering lines, and multi-pollutant retrofits | 90–99% | 20,000–1,200,000 Nm³/h | Gypsum or dry calcium residue | China GB 28662/GB 28663; project-specific emission standards |
Note: Supplier names are intentionally omitted. Technical ranges are indicative values commonly used for preliminary comparison; actual performance depends on fuel sulfur content, inlet dust loading, gas temperature, reagent quality, liquid-to-gas ratio, and applicable local emission limits.